Rounded corner flat bottom kettle — double flange
For baths of 2 m and under, where the flat base is the economical answer and the corner radii still do the work that matters.
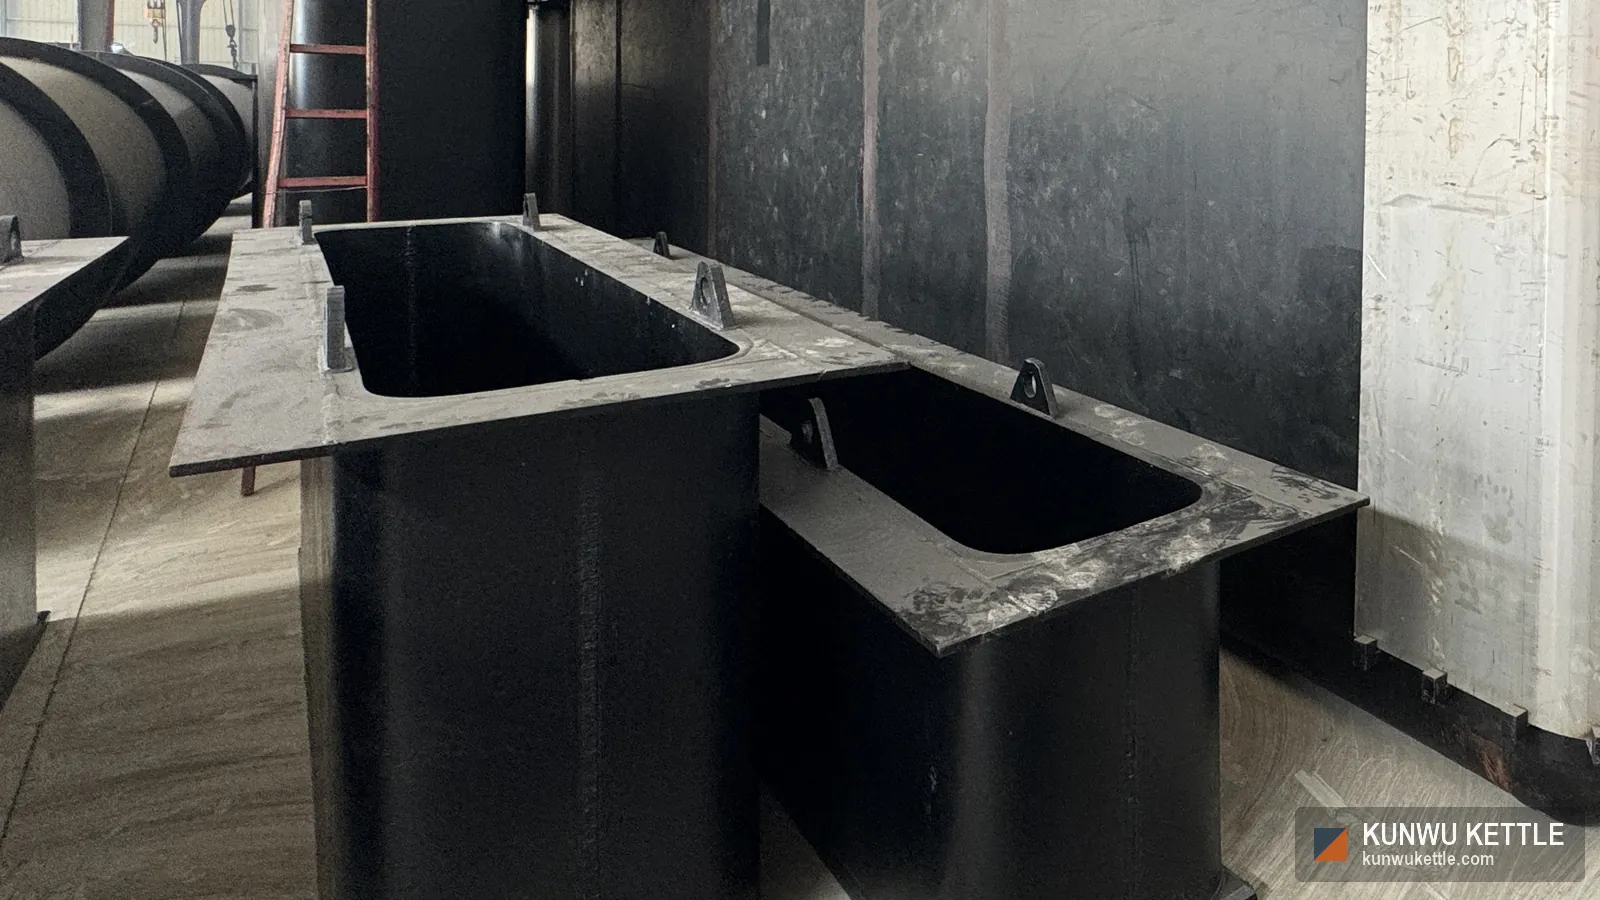
Why a flat bottom is the right answer under 2 m
Below 2 m of depth the hydrostatic load on the wall-to-base joint is modest, and the full radius stops earning its cost. What matters more at shallow depth is that the corners do not become dross traps and that corner zinc does not overheat.
Radiusing the wall-to-wall junctions handles both, while the flat base keeps the build simpler and the price lower. BG/T 1501-2015 Table 4 draws the line at 2 m, and so do we.
Bottom dross does settle in the base corners on this geometry — plan your skimming and dross removal accordingly. We can supply a dross shovel cut to your kettle’s corner radius.
Why double flange
Two flanges give the furnace a wider bearing surface and a stiffer top edge, which matters on long kettles where the top edge is the least supported part of the vessel.
If your furnace is built for a single flange, we build single. It is not a quality difference, it is an interface difference.
Specification
| Metric | Imperial | |
|---|---|---|
| Length | up to 16.5 m | up to 54 ft |
| Width | up to 3.6 m | up to 11.8 ft |
| Depth | up to 2.0 m | up to 6.6 ft |
| Wall thickness | 40 / 50 mm | 1.6 / 2.0 in |
| Corner radius | 125 – 200 mm | 4.9 – 7.9 in |
| Weight | 2 – 45 t | 2.2 – 50 short tons |
| Design standard | BG/T 1501-2015 |
Support note. Above 1.8 m depth the kettle needs one adjustable external support band; above 2.5 m, two. Support points at 1.5–2.0 m intervals, and expansion clearance along the length. Any part of the support inside the furnace hot zone must be heat-resisting steel. We specify this with the kettle.
Sizing this kettle for your plant
Three inputs decide it.
- Your largest workpieceSets minimum length and width, with clearance to dip, withdraw and skim.
- Your required throughputZinc volume should be 30–40× your maximum hourly throughput including jigs, so the bath temperature holds.
- DepthNormally 1.3–2× the width. Going deeper increases thermal mass, reduces temperature swing, lowers heat input density per m² of wall, and helps dross settle away from the work.
What every kettle gets
- Aluminium-killed low-silicon plate, Si ≤ 0.03 %Ultrasonically inspected plate-by-plate to GB/T 2970 Class III before cutting.
- All forming done warm, 850 – 900 °CCold bending locks residual stress into a vessel that will run at 450 °C for years.
- Electroslag welding, ISO 4063 process 72Full wall thickness in a single pass. No inter-pass interfaces.
- Weld metal specified to Si ≤ 0.03 %Grade 1 of BG/T 1501-2015 Table 10. Weld silicon decides where a kettle goes through first, so it is written into the order and evidenced by the welding consumable certificates that ship with the kettle.
- Ultrasonic testing of structural welds before dispatchGB/T 11345-2023 — identical (IDT) to ISO 17640:2018. Coverage and acceptance level are agreed with you and recorded in the inspection and test plan. Reports in English.
- No cruciform plate jointsParallel welds kept at least 0.5 m apart, per BG/T 1501-2015 §5.2.4.
- Full documentation packageIncluding the commissioning heat-up curve for your first firing.
Questions
Will dross build up in the base corners?
Some will. That is the trade-off for the flat base, and it is manageable with normal skimming practice. If your bath runs deeper than 2 m, take the full radius instead.
How long is the lead time?
It runs from confirmed drawings, not from your enquiry, and it depends on size and on what is already on the shop floor. We quote a date with the price, and we would rather quote a date we can hold than the shortest one that wins the enquiry. If you have a fixed outage window, tell us the date you need the kettle on site and we will tell you whether it is achievable before you place the order.
How is a kettle this size shipped?
Anything over about 12 m will not fit a standard container and moves on flat rack or as breakbulk. We arrange it — and we will tell you what your site needs to lift it off the truck before you order, not after.
Can you match our existing furnace?
Yes. Send the furnace opening dimensions, the support arrangement and how it is heated. Where a replacement has to drop into an existing furnace, the interface matters more than the catalogue.
Send three numbers, get a sized quote
Largest workpiece, required throughput, and how your furnace is heated. That is enough for us to come back with a sized kettle, a wall thickness, a zinc volume, a weight and a lead time.